

current collector metal etching
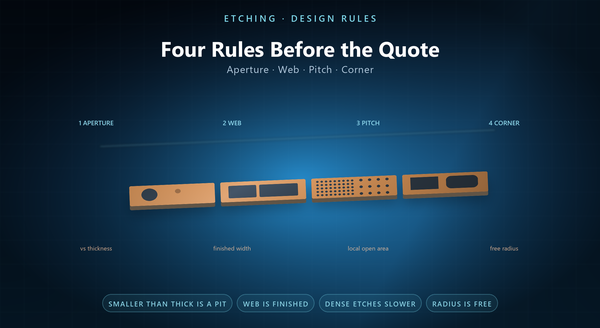
Current collector metal etching is worth judging before it is quoted, because most of the reasons a collector etch fails are visible on the drawing. The gauge, the smallest aperture, the web between apertures and the local open area decide most of the outcome, and they decide it in a way that can be checked in a few minutes rather than discovered after a week in the bath. This page is the entry point: what etching gives a collector, and the four rules that say whether a given design can have it.
1. What Etching Gives a Collector
Four things, and they are worth separating because a customer usually wants only one of them.
No burr. An etched edge has no burr on either face, which matters where the edge sits against a separator.
Pattern cost. The cost scales with panel area rather than with the number of apertures, so a dense field is cheap per hole.
No tooling. A change is a change to a file, so a prototype and a revision cost the same as a first article.
Thin gauge. Etching works at thicknesses where a die becomes difficult and a laser becomes a handling problem.
A design that needs none of those four is a design that should be cut rather than etched. A fifth reason is sometimes claimed, which is flatness, and it is worth treating with care: etching helps flatness by removing stress, and it does not guarantee it. A customer who asks for all four usually needs one, and knowing which one changes the design. A process that is chosen for the wrong reason is a process that will be judged on the wrong criterion.
2. Rule One: Aperture Against Thickness
The first rule is the ratio of the smallest aperture to the metal thickness.
Etching is isotropic, so a hole widens as it deepens: the etchant removes metal sideways at the same rate it removes it downwards. When the aperture is small relative to the thickness, the two sidewalls meet before the hole breaks through, and the feature never opens.
That is why every etch process has an aspect-ratio limit, and why a drawing that specifies a small hole in a thick foil is specifying a feature that will come out as a dimple rather than a hole. The rule is easy to apply: if the aperture is smaller than the thickness, ask before you design around it. A slot behaves better than a round hole at the same width, because the etchant has two long open ends to flow through. A round hole also has no straight wall to measure, which is why a slot is easier to accept as well as to etch. A hole that is at the limit of the process is also a hole whose tolerance is the first thing to be lost when the bath drifts.
3. Rule Two: Web Width
The second rule is the width of the metal left between two apertures.
A web is a ligament, and it has two jobs: it carries current and it holds the part together. An etched web is narrower than drawn, because the etch removes from both sides, and it is also thinner in section if the etch is two-sided.
Two things follow. A web should be specified as a finished width rather than a drawn one, and a web that is narrow relative to the thickness is a web that will be fragile before it is out of the bath.
There is no universal minimum, but the useful question is not “how narrow can you go” — it is “what happens to the part if this web is ten per cent narrower than drawn”. A web that carries current in a thin section is also a web that will heat, which is an electrical consequence of a mechanical dimension. A web that is uniform across the field is easier to etch than one that varies, because the local depletion is uniform too. A web also sets the open area, so the two rules are coupled and cannot be optimised separately.
4. Rule Three: Pitch and Open Area
The third rule is how close the apertures are, and it is a rule about flow rather than about strength.
Etchant has to reach every aperture and leave it, so a field that is dense in local terms etches more slowly than an isolated aperture, because the local chemistry is depleted. That is why a dense field and a sparse one on the same panel will not come out identical unless the artwork compensates for it.
Open area also sets the mechanical behaviour, because a high open area is a weak lattice. A field that is dense at one end of a panel and sparse at the other is a field where the panel’s position in the bath matters visibly. Open area is also the number that a coating process sees, because a coating bridges a small aperture more easily than a large one. A field that is dense and rectangular also cools and drains differently from a sparse one, which matters for a rinse. A design that wants both a very high open area and a stiff part is a design that needs a thicker foil or a different pattern, not a different etchant.
5. Rule Four: Corners and Radii
The fourth rule is the cheapest one, because etching gives good corners for free.
An etched inside corner is a radius that the process produces anyway, so a design that specifies a sharp internal corner is specifying something the process will approximate. A drawn radius that matches the process is a radius that can be inspected.
The same is true of outside corners: the etch rounds them slightly, which is usually an advantage because a sharp external corner on a foil is a handling hazard. A drawn sharp corner also makes a poor datum, because there is no measurable point to reference. A radius that is drawn smaller than the process can hold is a radius that will be argued about at inspection. A corner radius that is generous also strengthens the web at the corner, which is where a lattice usually fails first.
6. Tie Bars and Holding the Part
A collector is thin, so the question of how it is held during the etch is a design question, not a process detail.
A part is held by tie bars: narrow bridges of metal that connect it to the panel frame and are cut or broken at the end. The tie bar’s position decides whether the part is flat when it comes out, and its width decides whether it survives the rinse.
Two failures recur. A part that is held at one point will twist, and a part whose tie bars are too thin will be lost in the rinse rather than in the etch.
That is why a collector drawing should show the tie bar positions, or explicitly delegate them. A tie bar that is broken before the etch is a part that moves in the bath, and a moving part etches unevenly. A tie bar also leaves a witness mark where it is cut, which is a cosmetic question on a visible face. A part with many tie bars is a part that is flat but expensive to free, which is the trade.
7. The Four Questions
Four questions decide feasibility, and a supplier can answer all four without a sample.
What is the thickness? What is the smallest aperture, and is it a hole or a slot? What is the narrowest web, and does it carry current? And what is the tolerance on the functional dimension?
If the answers place the part inside the process, the next step is a first article. If they do not, the honest answer is a different process, and it is worth hearing that before a drawing is frozen. A fifth question is sometimes asked, which is about quantity, and it does not change feasibility, only the route. A sixth is about surface, and it is the one that decides whether the part can be coated afterwards. A seventh, if the part is new, is a photograph of the previous version, because it answers most of the rest.
8. What to Send
A quotable request for an etched collector has six items: the alloy and temper, the thickness, the pattern with the aperture and web dimensions, the functional dimension and its tolerance, the edge and surface requirements, and the quantity with its batch sizes.
It should also say whether the part has a coating face, because the etch leaves a surface and the coating will inherit it.
The recurring mistakes are an aperture smaller than the thickness with no note, A request that answers the four questions is a request that can be quoted in a day rather than in a fortnight. A request that names the coating face is a request that can be packed correctly as well as etched correctly. A request that names the batch sizes is a request that can be scheduled against a real capacity. a web specified as drawn rather than finished, a dense field with no compensation, tie bars left to the supplier without a flatness requirement, and a tolerance applied equally to every dimension.
